




The electric vehicle PCB assembly process converts a verified bare board and controlled component set into a programmed, inspected and tested electronic assembly. The basic SMT sequence resembles other PCBA production, but EV applications make thermal paths, high-current connections, vibration-sensitive parts, contamination control, traceability and test coverage more consequential. The correct controls depend on the board’s function, vehicle location and customer specification.
PCBTRY supports PCB fabrication, DFM review, component sourcing, assembly and testing as one controlled handoff. Send the Gerber data, BOM, placement file, drawings, firmware and acceptance requirements for an engineering review and quotation.
What Makes an Electric Vehicle PCB Assembly Different?
An EV assembly must be built around its actual electrical, thermal and mechanical duty. A low-voltage communication board, a battery-monitoring board and a high-power controller do not share one universal process window. The manufacturing plan should identify critical components, current paths, thermal interfaces, connector loads, test access and environmental protection before the first panel reaches the line.
How Does the Electric Vehicle PCB Assembly Process Work?
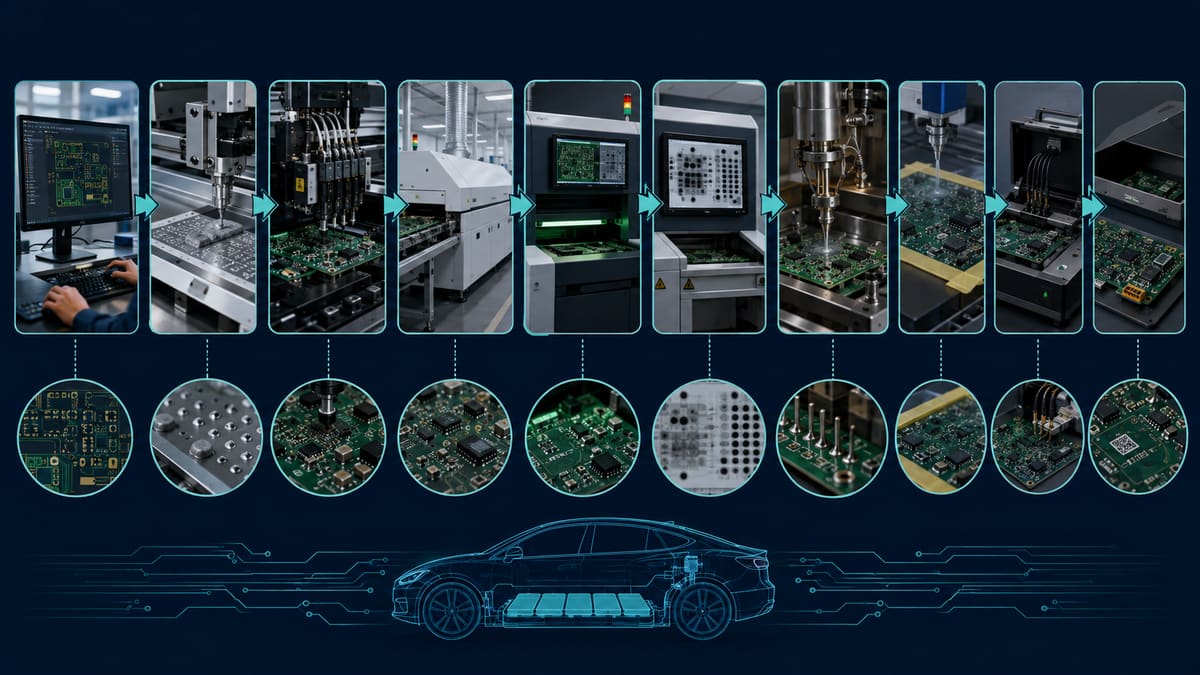
The process works as a controlled chain: every station receives defined inputs, creates measurable evidence and prevents defects from moving forward.
1. Engineering review and DFM/DFT analysis. Engineers compare Gerber data, drill files, BOM and centroid data, then review polarity, footprints, panelization, stencil access, test points, creepage constraints and mechanically loaded parts. Unresolved mismatches become wrong builds or untestable boards.
2. Bare-board and material verification. The incoming board revision, finish, thickness, copper requirements and electrical-test status are checked. Components are matched to approved manufacturer part numbers, lot data and moisture-handling requirements. A correct part in the wrong package or revision is still a line defect.
3. Solder-paste printing. Stencil design and printer setup control paste volume at fine-pitch devices, thermal pads and power terminals. Too little paste creates opens; excessive or uneven deposits raise bridge, void and tombstone risk.
4. SPI and component placement. Solder-paste inspection detects deposit problems before parts hide them. Pick-and-place programs must match centroid coordinates, package rotation, feeder data and polarity. First-article verification is where a mirrored coordinate system or wrong rotation should be contained.
5. Reflow soldering. The thermal profile must suit the paste, component mass, board construction and temperature-sensitive devices. Large copper regions and heavy components can heat differently from small signal parts, so a copied profile may leave cold joints or overheat sensitive packages.
6. AOI and X-ray inspection. AOI checks visible polarity, placement and solder features. X-ray is selected for hidden joints such as BGA, QFN thermal pads or other inaccessible connections. Neither method proves circuit function, so inspection criteria must connect to later electrical tests.
7. Through-hole and selective soldering. Connectors, relays, transformers and other leaded parts may require selective soldering, wave soldering or controlled hand work. The key risks are incomplete barrel fill, bridges, heat exposure and mechanical load transferred into solder joints.
8. Cleaning, coating and mechanical reinforcement. Cleaning requirements depend on flux chemistry and protection strategy. Conformal coating or staking is applied only after the assembly and masking plan are verified; coating over contamination or untested hardware can lock in a reliability or rework problem.
9. Programming and electrical testing. Programming, ICT, flying-probe access, boundary scan or functional tests are selected by coverage need and volume. The test must verify the faults that matter—not merely that the board powers on.
10. Final inspection and release. The supplier confirms workmanship, labels, revision, serialized records, test result and packaging. Release evidence should link the shipped assembly to the approved files, material lots and process history.
Which Materials and Components Need Extra Control?
| Item | Assembly concern | Buyer evidence to request |
|---|---|---|
| Power semiconductors | Thermal-pad soldering, voiding and heat removal | Approved footprint, X-ray criteria and thermal-interface plan |
| Large connectors | Barrel fill, coplanarity and insertion force | First-article images and mechanical support method |
| Magnetics and capacitors | Mass, vibration load and polarity | Placement/reinforcement drawing and inspection criteria |
| Moisture-sensitive packages | Storage, floor life and reflow damage | Handling and lot records appropriate to the part |
| Coating or potting material | Compatibility, masking, cure and rework | Material approval, keepout map and inspection method |
How Should DFM and DFT Be Planned?
DFM decides whether the board can be assembled repeatedly; DFT decides whether faults can be found economically. Review stencil apertures, component spacing, polarity visibility, rework access and panel support together with probe access, programming connectors and measurable test limits. A test point that exists in CAD but is blocked by a connector or coating mask has no production value.
What Are the Main EV PCBA Failure Risks?
| Risk | Typical mechanism | Prevention or containment |
|---|---|---|
| Thermal fatigue | Expansion mismatch stresses joints and pads | Review materials, package geometry, heat paths and validation profile |
| Vibration damage | Heavy parts or cables load component leads | Add mechanical support and verify fixture/enclosure loads |
| Contamination | Residue plus moisture drives leakage or corrosion | Control cleaning, handling and coating preparation |
| Latent solder defects | Poor paste transfer, profile or hidden-joint voiding | Combine SPI, profile evidence, AOI/X-ray and electrical test |
| Revision escape | Wrong BOM, firmware or placement data reaches production | Use controlled release packages and serialized traceability |
How Are Soldering Profiles and Thermal Paths Controlled?
Profile control begins with the actual populated board. Thermocouples should represent high-mass, low-mass and sensitive locations, and the result should be judged against the approved paste and component constraints. For power assemblies, solder quality alone is insufficient: copper spreading, thermal vias, interface materials, heatsink flatness and fastener loads can all change junction temperature and reliability.
What Inspection and Tests Should Be Used?
No single test covers workmanship, connectivity, firmware and load behavior. Build a test stack around failure coverage.
| Method | Finds well | Does not prove |
|---|---|---|
| SPI | Paste volume, height and alignment | Final solder-joint or circuit function |
| AOI | Visible placement, polarity and solder anomalies | Hidden-joint integrity or firmware behavior |
| X-ray | Hidden connections, void patterns and bridges | Electrical performance by itself |
| ICT/flying probe | Opens, shorts and selected component values | Complete behavior under real load |
| Functional test | Interfaces, firmware and defined operating states | Every latent environmental failure |
| Environmental validation | Project-defined thermal, vibration or humidity response | Universal lifetime without a valid mission profile |
Why Do Traceability and Change Control Matter?
Traceability connects a serial number to its PCB revision, component lots, operators or line, program version, inspection data and test result. This lets a team contain a suspect population rather than treating every shipped board as equally affected. Change control must also define what requires customer approval: substitute parts, stencil changes, repair methods, firmware and process deviations can change reliability even when the part number on the shipment stays the same.
How Do Pilot Builds Reduce Production Risk?
A pilot build validates the release package and the production route before volume amplifies mistakes. Use it to close first-article findings, tune profiles, confirm test limits, measure defect patterns and verify traceability. The output should be an approved build record and open-issue list, not simply a few working samples.
How Long Does EV PCB Assembly Take?
Lead time depends on component availability, PCB construction, tooling, process validation, test-fixture readiness, coating/cure steps and approval loops. Ask suppliers to separate material procurement, fabrication, assembly, engineering hold points and customer approval time. An urgent build without frozen files or a ready test plan often waits at an engineering gate rather than on the SMT line.
How Do You Choose an EV PCB Assembly Supplier?
Compare evidence that matches your product. Ask how the supplier controls revisions, substitutes, moisture-sensitive parts, paste printing, thermal profiling, hidden joints, heavy components, cleanliness, coating masks, programming and test data. Also ask who owns failure analysis and how nonconforming material is contained.
- Can the supplier review Gerber, BOM and placement data as one controlled set?
- Which inspection and test stages map to your critical failure modes?
- How are serial numbers linked to materials, firmware and test records?
- Which processes are in-house and which require an approved external source?
- What evidence is delivered with prototypes, pilots and production lots?
Frequently Asked Questions
What files are needed for an EV PCB assembly quote?
Provide Gerber or ODB++ data, drill files, BOM, pick-and-place data, assembly drawings, quantity and board specifications. Add firmware, programming instructions, test requirements and coating/masking drawings when applicable.
Is AOI enough for EV PCB assembly?
No. AOI examines visible features, but it cannot fully assess hidden joints or prove electrical function. Combine inspection and electrical testing according to package type and failure risk.
When is X-ray inspection needed?
Use X-ray where important solder joints are hidden or visual access is inadequate, such as under BGA or QFN packages. Define acceptance criteria before production rather than judging images subjectively afterward.
Should conformal coating be applied before functional testing?
Normally the process should confirm assembly function and cleanliness before coating, while the final control plan may include post-coating checks. The exact sequence depends on masking, test access and customer requirements.
How are heavy components protected from vibration?
The design should keep solder joints from carrying unsupported mass or cable loads. Mechanical fixtures, approved staking or enclosure support must be evaluated with material compatibility and rework needs.
What is the difference between component qualification and PCBA validation?
A qualified component has passed its defined qualification regime; that does not automatically validate its solder joint, layout, cooling or behavior in your assembly. Board-level and system-level validation still follow the product mission profile.
What should a pilot build report include?
It should identify file revisions, material deviations, first-article results, process settings, inspection/test results, defects, repairs and open actions. Agree on the evidence package before the build.
Can one EV test plan fit every board?
No. Coverage must reflect the board function, safety impact, interfaces, environment and customer specification. Reuse test architecture where helpful, but validate the limits for each design.
Prepare the EV PCBA Package for Engineering Review
Send PCBTRY the controlled fabrication data, BOM, centroid file, drawings, firmware, quantities and acceptance criteria. Include the vehicle location, electrical load, thermal interface, coating needs and required test evidence so the quotation reflects the real process rather than an assumed generic assembly.



0 Comments