




In an OEM vs supplier relationship, the chief engineer should keep final authority over product intent, engineering risk, design changes, and release approval, while the supplier should control manufacturing execution within approved requirements. The healthiest projects do not treat the supplier as a silent order taker or let the supplier override design authority; they define where advice ends, where approval begins, and what evidence is required before a decision becomes official.
What Chief Engineer Decision-Making Power Means in OEM vs Supplier Work
Chief engineer decision-making power means the authority to accept or reject technical risk on behalf of the product, not simply the authority to overrule everyone else. In OEM manufacturing, that authority usually covers product function, design intent, performance targets, reliability expectations, compliance needs, critical materials, engineering changes, validation plans, and production release conditions.
The supplier’s role is different but still technical. A strong PCB, PCBA, mechanical, or contract manufacturing supplier should challenge weak designs, warn about process limits, recommend DFM changes, and stop production when requirements cannot be met. The supplier’s influence is essential, but it should be converted into controlled decisions through drawings, specifications, engineering change orders, test reports, and written approval.
OEM vs Supplier: The Practical Difference in Authority
The OEM owns what the product must do, while the supplier owns how approved requirements can be manufactured repeatably. This difference sounds simple, but many project delays come from confusing product authority with process authority.
| Decision Area | OEM Chief Engineer Authority | Supplier Authority | Shared Evidence Needed |
|---|---|---|---|
| Product function | Defines required performance and risk limits | Reviews whether design can be built and tested | Specification, schematic, layout files, test plan |
| DFM changes | Approves changes that affect fit, function, reliability, or compliance | Proposes manufacturability improvements | DFM report, risk note, revised drawing |
| Process routing | Defines requirements and special controls | Selects practical manufacturing process route | Control plan, process traveler, inspection record |
| Material substitution | Approves if material affects performance, reliability, safety, or compliance | Suggests available alternatives and supply risks | Datasheet, equivalency review, validation result |
| Quality acceptance | Defines acceptance criteria and customer risk | Inspects, reports, and holds nonconforming lots | Inspection standard, COC, test data, nonconformance report |
Why Decision Boundaries Matter More Than Job Titles
Decision boundaries prevent hidden design changes, uncontrolled cost cuts, unclear responsibility, and late-stage quality disputes. A chief engineer with no supplier input can approve a design that is technically elegant but difficult to build. A supplier with too much informal influence can make small process-friendly changes that create field risk later.
Good boundaries are especially important in PCB and PCBA projects because small details can affect yield, reliability, and assembly quality. Examples include copper balance, annular ring, impedance tolerance, solder mask clearance, via plugging, component substitution, thermal relief, stencil aperture design, reflow profile, cleaning requirements, and electrical test coverage. Some of these are supplier process choices; others affect the product design and require OEM approval.
A Clear Decision Matrix for OEM and Supplier Teams
A decision matrix should define who recommends, who approves, who executes, and who keeps records before the project reaches production. The table below can be adapted for PCB/PCBA, mechanical parts, cable assemblies, and complete electronic assemblies.
| Topic | Recommend | Approve | Execute | Record |
|---|---|---|---|---|
| PCB stack-up adjustment | Supplier or OEM engineer | OEM chief engineer if electrical, mechanical, or reliability impact exists | Supplier | Approved stack-up, impedance target, drawing revision |
| Component substitution | Supplier or purchasing team | OEM engineering and quality teams | Supplier after approval | AVL update, datasheet comparison, validation evidence |
| Panelization and tooling | Supplier | Supplier, unless product constraints are affected | Supplier | Panel drawing, tooling confirmation |
| Critical test method | OEM and supplier jointly | OEM chief engineer for release criteria | Supplier or test partner | Test procedure, fixture record, test data |
| Production lot release | Supplier quality team | Supplier for normal release; OEM for deviation or concession | Supplier | Inspection report, COC, deviation approval if needed |
Where Suppliers Should Challenge the OEM
A supplier should challenge the OEM when the design creates avoidable manufacturing risk, unclear inspection criteria, unstable yield, or quality exposure. This is not a power struggle; it is one of the supplier’s most valuable technical contributions.
- DFM risks: trace/space limits, drill-to-copper clearance, solder mask slivers, warpage risk, poor copper balance, or unrealistic impedance tolerance.
- Assembly risks: insufficient component spacing, tombstoning risk, thermal mismatch, BGA inspection limitations, stencil design concerns, or reflow sensitivity.
- Test risks: incomplete test coverage, unrealistic pass/fail criteria, missing boundary-scan access, unclear ICT fixture requirements, or no golden sample plan.
- Supply-chain risks: long-lead components, obsolete parts, unapproved alternates, inconsistent laminate availability, or packaging constraints.
- Documentation risks: mismatched Gerber, drill, BOM, centroid, assembly drawing, revision, and acceptance criteria.
The supplier should present these issues with evidence: risk description, affected requirement, proposed option, expected benefit, trade-off, and whether OEM approval is required. Vague statements such as “hard to make” or “we usually change this” are not enough for controlled engineering decisions.
Where the Chief Engineer Should Not Delegate Final Approval
The chief engineer should not delegate final approval for any change that could affect product performance, field reliability, compliance, safety, user experience, or customer acceptance. Delegation is useful for execution; it is dangerous when it hides risk ownership.
- Changing a PCB stack-up that affects impedance, dielectric thickness, thermal behavior, or mechanical fit.
- Replacing a component with different electrical, thermal, lifecycle, package, or certification characteristics.
- Relaxing inspection or test criteria because production yield is low.
- Accepting a deviation for a critical parameter without documented engineering risk review.
- Changing surface finish, laminate, copper weight, solder paste, conformal coating, or cleaning requirements when reliability may be affected.
- Approving pilot-run results without reviewing failures, rework, yield data, and open corrective actions.
How Engineering Change Control Should Work
Engineering change control should turn supplier feedback into traceable decisions before procurement, production, or quality release is affected. A practical change workflow keeps the supplier fast without allowing uncontrolled changes.
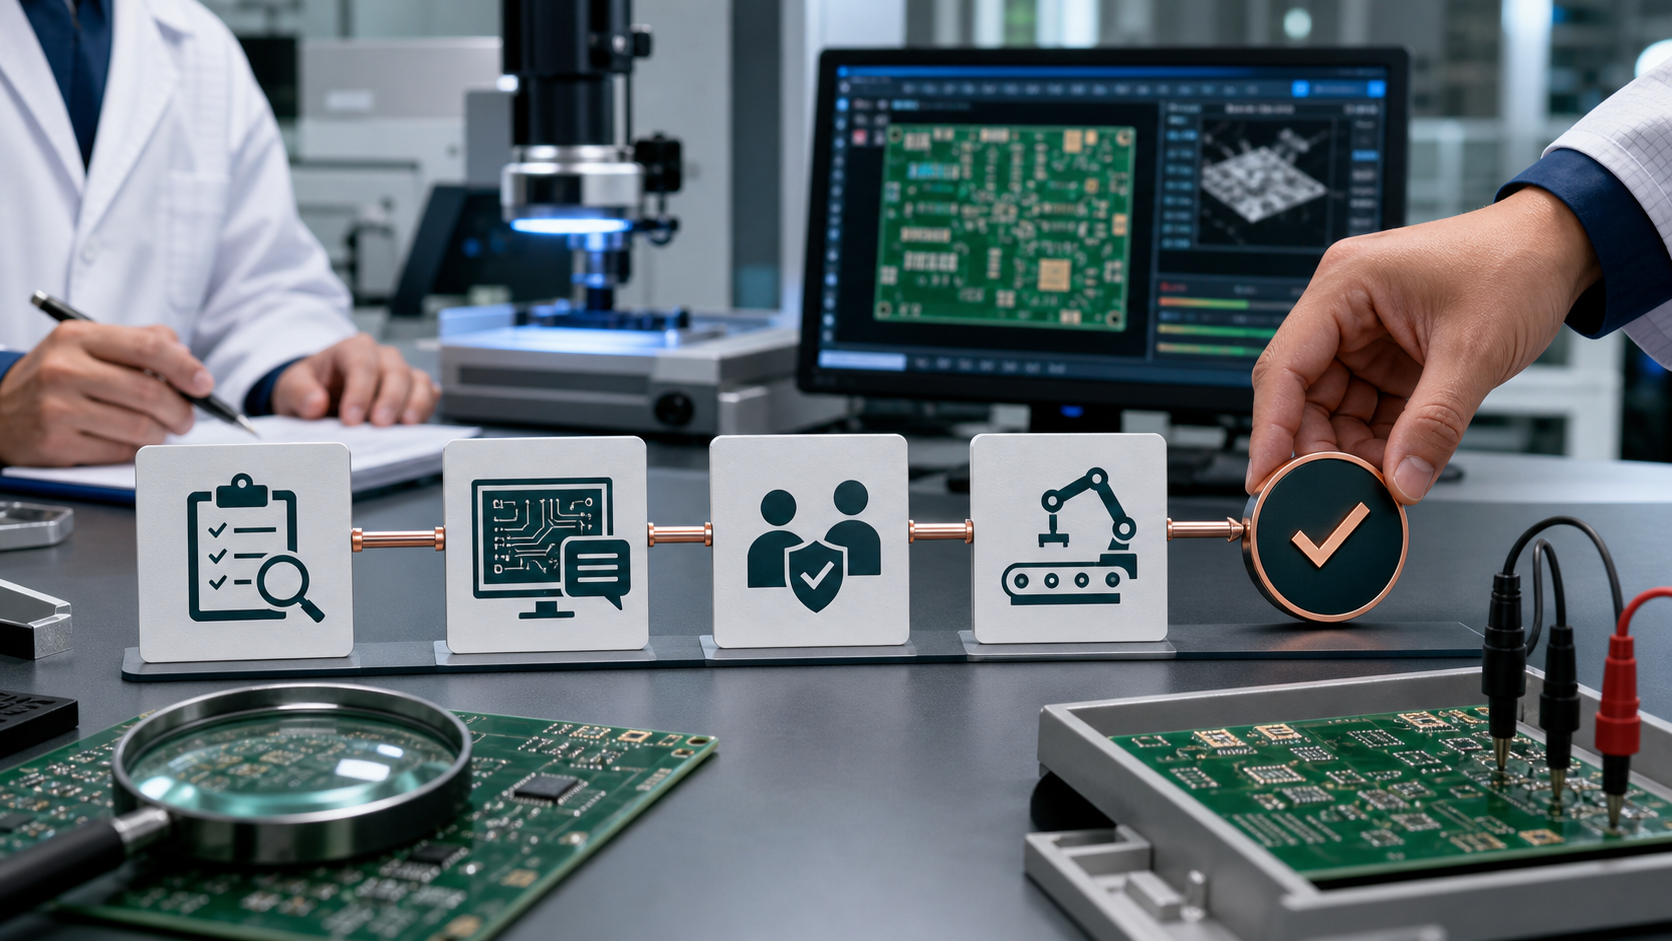
- Supplier identifies a risk or improvement opportunity during quotation, DFM review, sample build, pilot run, or mass production.
- Supplier documents the issue, affected drawing or specification, proposed change, expected benefit, and possible risk.
- OEM engineering classifies the change as minor, major, safety/compliance-related, or customer-impacting.
- Chief engineer approves, rejects, or requests validation based on product risk.
- Supplier implements only the approved revision and keeps process records aligned with the latest document package.
- Quality team verifies samples, test data, first article results, or production lot evidence before release.
Quality Standards and Acceptance Criteria
Standards are useful only when the OEM and supplier agree which ones apply, which class level is required, and which customer-specific requirements override general practice. In PCB and PCBA projects, buyers often reference IPC standards for board and assembly acceptance, while automotive-style programs may also use APQP, PPAP, FMEA, control plans, MSA, and SPC when required by the customer.
Do not assume that naming a standard solves the decision problem. The chief engineer should still define critical parameters, approved deviations, special characteristics, sample size, test coverage, documentation needs, and escalation rules. The supplier should provide inspection and process evidence that maps to those requirements.
| Control Item | Chief Engineer Question | Supplier Evidence |
|---|---|---|
| Incoming materials | Are material requirements and alternates approved? | Material certificate, approved vendor list, traceability record |
| First article or sample | Does the sample prove design and process readiness? | FAI report, dimensional check, electrical test, visual inspection |
| Process capability | Can critical parameters be held in production? | Control plan, SPC data when required, process audit result |
| Assembly quality | Are soldering and placement criteria defined? | AOI, X-ray when needed, functional test, IPC acceptance reference |
| Deviation handling | Who accepts risk for this specific lot? | Deviation request, root-cause note, containment and approval record |
Common Failure Modes When Power Is Unclear
Unclear decision power usually appears first as small shortcuts and later as delivery delays, quality disputes, or field failures. The problem is rarely one bad decision; it is often a chain of informal decisions that were never reviewed by the right owner.
- Supplier changes a material to meet lead time, but the OEM later finds reliability or compliance risk.
- OEM approves a tight tolerance without asking whether the supplier can hold it at mass production scale.
- Purchasing accepts a lower-cost option without engineering review.
- Supplier waives an inspection item because it is difficult to measure consistently.
- Engineering releases a revision, but the supplier builds from an older Gerber, BOM, drawing, or test instruction.
- Quality rejects a lot using criteria that were not defined in the purchase package.
Supplier Selection Questions for Chief Engineers
The best supplier for a chief engineer is not simply the cheapest supplier; it is the supplier that can separate advice, approval, execution, and evidence. Use supplier selection questions that reveal decision discipline, not only capability lists.
- How do you document DFM findings before sample production?
- Which changes require written OEM approval before production?
- How do you prevent production from using outdated files?
- What inspection data do you provide with samples and mass production lots?
- How do you handle nonconforming product, deviations, concessions, and lot holds?
- Can your engineering team explain the trade-off behind each DFM recommendation?
- How do you manage component substitutions or laminate availability changes?
- What is your escalation process when cost, lead time, and engineering risk conflict?
Cost, Lead Time, and Decision Power Trade-Offs
Cost and lead time pressure should influence engineering decisions, but they should not bypass engineering authority. In real projects, the cheapest or fastest option may be correct if the risk is low and evidence is strong; it is dangerous when the option quietly changes requirements.
| Pressure | Supplier May Suggest | Chief Engineer Should Check | Decision Rule |
|---|---|---|---|
| Lower PCB cost | Panel optimization, stack-up simplification, surface finish alternative | Signal integrity, assembly compatibility, reliability, storage life | Approve only if product risk is unchanged or validated |
| Shorter lead time | Available laminate, substitute component, partial test plan | Compliance, lifecycle, electrical fit, test coverage | Use written temporary approval when risk is bounded |
| Higher yield | Relaxed tolerance or modified process window | Customer requirement and functional impact | Do not relax CTQ items without engineering review |
| Mass production ramp | Process automation or tooling change | Repeatability, first article evidence, revalidation need | Approve through change control if output may change |
Pre-Order Checklist Before Giving a Supplier Manufacturing Freedom
Before a supplier receives broad manufacturing freedom, the chief engineer should make sure the technical package, approval rules, and escalation paths are complete. This checklist reduces ambiguity before cost and delivery pressure appear.
- Latest controlled revision of drawings, Gerbers, drill files, BOM, centroid file, assembly drawings, and test requirements.
- Critical-to-quality parameters clearly marked, including any no-change items.
- Approved material list, component alternates, and substitution approval process.
- DFM response loop completed before tooling or mass production.
- Sample approval criteria defined before samples are built.
- Inspection and test requirements matched to the product risk level.
- Deviation and concession approval route agreed in writing.
- Packaging, labeling, traceability, and documentation expectations confirmed.
- Production hold authority defined for supplier quality and OEM engineering.
- Escalation contact path available for urgent technical decisions.
FAQ
Who has final decision-making power in an OEM vs supplier project?
The OEM normally has final decision-making power over product requirements, design intent, qualification criteria, and release approval. The supplier should have decision rights over process control, manufacturing method recommendations, and reject/hold actions when requirements cannot be met safely.
Can a supplier change an OEM design?
A supplier should not change the OEM design without written approval. A strong supplier can propose DFM, material, stack-up, tolerance, or test changes, but the OEM chief engineer should approve changes that affect fit, function, reliability, compliance, or product documentation.
What should the chief engineer control directly?
The chief engineer should directly control design requirements, critical-to-quality parameters, risk acceptance, engineering change approval, validation evidence, and final release criteria. Routine production methods can be delegated if the acceptance criteria are clear.
What decisions should the PCB supplier own?
The PCB supplier should own process routing, panelization suggestions, manufacturability feedback, in-process inspection methods, process capability alerts, and production hold recommendations. These decisions must still align with the OEM specification and approved drawings.
Why do OEM and supplier conflicts happen?
Conflicts usually happen because design authority, cost pressure, test standards, change approval, or acceptance criteria were not defined early. A supplier may optimize for yield and manufacturability while the OEM protects product function, compliance, and customer risk.
Should purchasing decide between OEM requirements and supplier recommendations?
Purchasing can compare cost, lead time, payment terms, and commercial risk, but technical trade-offs should go through engineering review. If a supplier recommendation changes product requirements or quality risk, the chief engineer should approve it before purchasing commits.
How early should the supplier join the engineering decision process?
The supplier should join before tooling, sample builds, and final release whenever manufacturability matters. Early DFM review is especially valuable for PCB stack-up, impedance, material selection, component availability, assembly constraints, test access, and quality documentation.
What is the difference between supplier advice and supplier approval?
Supplier advice is a technical recommendation based on manufacturing experience. Supplier approval means the supplier accepts responsibility for building to the agreed requirement. OEM approval is still needed when the recommendation changes design intent, acceptance criteria, or product risk.
How should OEMs handle supplier DFM recommendations?
OEMs should require each DFM recommendation to state the issue, affected requirement, proposed change, benefit, risk, and approval need. The chief engineer can then approve low-risk improvements quickly and require validation for changes that affect performance or reliability.
When should a supplier stop production?
A supplier should stop production when the approved requirement cannot be met, files conflict, material is unavailable, test results fail, a critical process drifts out of control, or a deviation has not been approved. Stop authority should be defined before mass production.
Does the chief engineer need to approve every production detail?
No. The chief engineer does not need to approve routine process settings, operator assignments, normal inspection flow, or standard production routing if the supplier can meet approved requirements. The chief engineer should focus on requirements, risk, changes, validation, and release decisions.
How can an OEM avoid uncontrolled supplier changes?
The OEM should issue controlled document packages, mark critical requirements, define no-change items, require written approval for substitutions, review DFM reports, and audit sample or production evidence. Clear revision control is often the simplest protection against uncontrolled change.
Final Takeaway for Chief Engineers
Chief engineer decision-making power in OEM vs supplier work should be strong, but it should also be structured enough to use supplier expertise. Keep final authority over product risk, design changes, validation, and release approval. Give the supplier enough authority to control process execution, raise risks, stop unsafe production, and provide evidence. The result is faster manufacturing without losing engineering control.
If you’re sourcing reliable PCB/PCBA manufacturing, including OEM, ODM, prototyping, mass production, or custom engineering solutions, reach out to our engineering team for technical support and a quote at [email protected]



0 Comments